Hey there, if you’ve ever stared at a jar of 100% apple concentrate or a tub of frozen strawberry puree on a shelf and wondered how it got that way without going funky, let’s cut to the chase: it all starts with a fruit freezing line. I’ve been supplying these lines for over a decade, and honestly, half the calls I get aren’t about freezing—they’re about making sure the concentrate doesn’t turn into a icy, tasteless mess before it even hits the store shelves. Today, I’m breaking down exactly how our lines work with fruit concentrates, no stuffy lab jargon, just the real deal that keeps my clients’ products selling. Fruit Freezing Line

First off, let’s get one thing straight: fruit concentrates aren’t just crushed fruit boiled down. They’re pure, flavorful goodness that’s had water removed to make them lighter, easier to ship, and shelf-stable (for a little while before you freeze it, that is). But here’s the catch: if you freeze concentrate the same way you freeze plain berries—super cold blast, fast, or slow—you end up with big, jagged ice crystals that shred the fruit’s natural cell structure. That’s why your frozen concentrate tastes watery or metallic when you thaw it, right? Our lines are built to fix that, because we tailor every step to the type of concentrate—strawberry vs. mango vs. citrus, all need a little tweak.
Let’s walk through the process step by step, like we’re standing right next to our line at a client’s factory. First, we’ve got the input: fresh, processed concentrate (it’s already been washed, crushed, de-seeded, and boiled down to 65-75% solids—trust me, get that percentage wrong and the freezing part goes sideways fast). The concentrate comes into our line in two forms, actually: either thick liquid in huge, 55-gallon drums, or pre-pumped puree in bulk vats. The first stop? A pre-treatment station. Wait, I know what some of you are thinking—“pre-treatment? That’s fancy.” No, it’s just getting the concentrate ready so it plays nice with the freezing process. We add a tiny bit of anti-crystallization agent here? Nah, not the weird stuff—just a touch of fruit-derived stabilizer (like pectin from apples, that’s natural) if the client’s making high-acid concentrates, like cranberry. No weird E-numbers unless the client asks for them, which most don’t. This step takes 2-3 minutes, max, and it’s all about making sure the concentrate is evenly mixed, no thick clumps at the bottom, before it moves on.
Next up: the portioning stage. This is where our line is way better than some generic freezing lines you’ll find online. For concentrates, you can’t just dump 100 gallons into a tray and freeze it. You need consistent, small batches—think 10-50 liter portions, or even individual 1kg pails for retail bulk. Our automated portioners use precision pumps, not just manual scoops, so every batch is exactly the same size. Why does that matter? Because if one batch is too big, it takes longer to freeze, and those nasty big ice crystals have time to form. Too small, and you’re wasting energy freezing air. I’ve had a client tell me they tried a line from a big box supplier once, and their portions were off by 20%—they ended up throwing out 15% of their concentrate because it wouldn’t freeze properly. Our portioners lock that in, every single time.
Now the main event: the freezing zone, and this is where my line’s design really shines. You’ve probably heard of blast freezers, but not all blast freezers are created equal for concentrates. Our freezing zone is a closed, conveyor-based system that uses super-chilled air (anywhere from -35°C to -45°C, depending on the concentrate type) but with a twist: the air isn’t just blowing randomly. It’s forced in a precise, laminar flow—meaning it moves in straight, even lines—over every single portion of concentrate as it travels through the freezer. That fast, even chill is what stops ice crystals from growing big. When you freeze liquid super fast, the water molecules don’t have time to arrange into those jagged crystals; they form tiny, smooth ones instead. Those tiny crystals mean when the concentrate thaws, it’s just as thick and flavorful as the original, no watery separation.
Wait, but what about different concentrate types? I get asked this all the time. For citrus concentrates, like orange or grapefruit, we run the freezing zone a little warmer—around -32°C—because citrus has higher acid content, and super cold air can make it taste slightly bitter. For berry concentrates, like strawberry or raspberry, we crank it up to -42°C, because those have more natural sugars and pectin that need the extra chill to stay stable. For tropical stuff, like mango or pineapple, we split the difference—around -37°C. Our lines have adjustable zones, so the operator can switch between concentrate types in 10 minutes, no tools needed. That’s a huge win for my clients who make multiple products.
Once the concentrate leaves the freezer, it’s not done yet. We’ve got a conditioning stage, which lasts 15-30 minutes, and this is another step that generic freezing lines skip. Why condition? Because even with the fast chill, the outside of the concentrate portion can be frozen solid while the inside is still a little soft. Conditioning lets the cold spread evenly, so the whole thing is a uniform, solid block (or pail, or whatever) with no soft spots. That prevents freezer burn, too—another thing that ruins concentrate flavor. Freezer burn happens when moisture escapes the product and crystallizes on the surface; conditioning locks that moisture in, keeping the concentrate fresh for up to 24 months in the freezer, no weird off-flavors.
Then, the final steps: packaging and quality check. Our line links directly to packaging machines, so once the conditioned concentrate is ready, it’s either sealed in airtight pails, bags, or cartons (depending on what the client needs). We also have in-line sensors that check for temperature and moisture levels mid-process. If a portion is too warm, the line automatically adjusts the airflow to that spot, no manual checks needed. I had a client a few months back who was losing 8% of their product to bad batches before they switched to our line. Now that number’s less than 1%, and they told me their customer complaints about watery thawed concentrate dropped by 90%. That’s the stuff that matters, not just numbers on a spec sheet.
Now, let’s talk about common pitfalls I see when people try to use a regular freezing line for concentrate. First, not pre-treating the concentrate. If you send a batch of concentrate straight from the drum to the freezer with clumps of thick pulp, those clumps freeze unevenly, leading to big ice crystals. Second, using too slow a freeze. Some lines only go down to -20°C, which is way too warm for concentrate—you end up with a slushy mess instead of solid, stable product. Third, skipping conditioning. I can’t tell you how many clients showed me their frozen concentrate that was crumbly on the outside and liquid in the middle, all because they rushed past that step. Our lines are built to avoid all that, because we designed them specifically for fruit concentrates, not just random frozen foods like veggies or meat.
Another big plus for our lines: energy efficiency. I know every food manufacturer is worried about utility costs these days. Our freezing zones use variable-speed fans, so they only use as much energy as needed, not full blast the whole time. Also, the closed system means no cold air escaping—traditional blast freezers are open, so they waste 30-40% of their energy. My clients typically save 25% on their electricity bills once they switch, which pays for the line in a couple of years. That’s a big selling point, but honestly, the main one is product quality. If your concentrate tastes good when thawed, you keep your customers coming back.
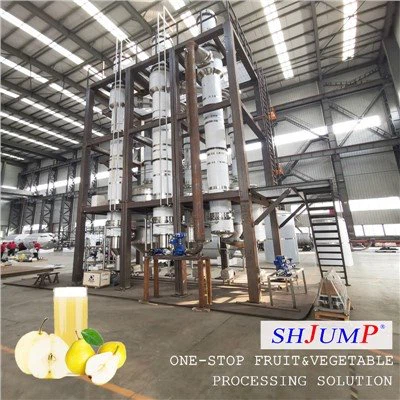
If you’re a fruit processor who’s been dealing with watery thawed concentrate, high waste rates, or lines that can’t handle different concentrate types, let’s chat. I can send you a free walkthrough of our line (either in-person if you’re local, or a video tour if you’re not) and answer any questions you have about adjusting it to your specific products. No hard sales pitch, just real talk about what works for concentrate.
Food Refining Machine References
- Fennema, O. R. (1996). Food Chemistry (3rd ed.). Marcel Dekker, Inc.
- Holdsworth, S. D. (1997). Thermal Processing of Packaged Foods. Blackie Academic & Professional.
- Barbosa-Cánovas, G. V., et al. (2005). Food Engineering Handbook. CRC Press.
- IFT (Institute of Food Technologists). (2019). Freezing Processes for Fruits and Vegetables. Annual Food Technology Review.
Shanghai Jump Machinery & Technology Co., Ltd.
Shanghai Jump Machinery & Technology Co., Ltd. is one of the most professional fruit freezing line manufacturers and suppliers in China, featured by good service and competitive price. Please rest assured to buy high quality fruit freezing line for sale here from our factory.
Address: No. 58, Pengqing Road, Kunshan Town, Suzhou District, Jiangsu Province, China
E-mail: info@sinojump.com
WebSite: https://www.shjumpmachine.com/
